

In recent years, the industry's attention to the global hot melt welding standard system has continued to rise. To help its partners and industry colleagues accurately grasp the standard requirements, Saemin welding machines have specially sorted out the mainstream global hot melt welding standards and their corresponding core parameters, providing authoritative references for engineering practice.
As the benchmark framework in the global hot melt welding field, the series of standards of the International Organization for Standardization (ISO) have laid the foundation for industry norms. The ISO certificate of Saemin hot melt welding machine updated last week has just been issued.
Among them, ISO 12176-1 "Plastic pipes and fittings - polyethylene system welding equipment - Part 1: "Hot Melt Butt Welding" clearly defines the performance requirements, test methods and working environment boundaries of PE pipe hot melt butt welding equipment. It stipulates that the normal working environment temperature of the equipment should be controlled within -10℃ to +40℃, and the temperature stability error of the heating plate should not exceed ±3℃. This standard is also an important reference blue for the Chinese standard GB/T 20674.1-2006. Another core international standard, ISO 21307:2017, has detailed the operation norms for three butt welding processes of PE pipes (single low pressure, double low pressure, and single high pressure), providing differentiated parameters for pipes of different wall thicknesses: the temperature of the heating plate for single low pressure butt welding is 225±10℃, and the pressure is 0.17±0.02MPa. For double low-pressure fusion welding (applicable to pipes with wall thickness > 22mm), the temperature of the heating plate should be 232.5±7.5℃, and the pressure should be gradually reduced from 0.15MPa to 0.025MPa. Single high-pressure welding adopts a combination of a heating temperature of 215±15℃ and a pressure of 0.52±0.1MPa, effectively meeting the welding requirements under different working conditions.
At the regional standard level, the standard systems of the mainstream industrial countries in Europe and America are each distinctive and highly targeted. ASTM F2620 of the United States, "Specification for Hot Melt Connection of Polyethylene Pipes and Fittings", focuses on high-pressure scenarios such as gas and drinking water. Besides clearly stating the heating temperature range of 210-230℃, it also puts forward strict requirements for the pressure test after welding - it needs to maintain no leakage for 24 hours at 2.5 times the maximum working pressure. At the same time, it is stipulated that the pressure control accuracy of large-diameter pipes with a diameter of DN200 and above should reach ±0.1MPa. The Saemin hot melt welding machine used the ASTM standard test of the United States in the 315 Elbow, tee and cross multi-angle welding machine video customized for the American customer.
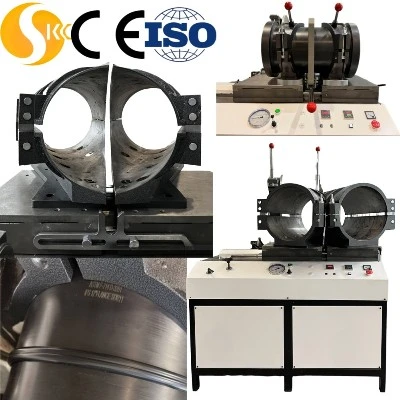

The German DVS series standards are renowned for their high precision. DVS 2207-1 covers the hot melt welding process of multiple material pipes and plates such as PE63, PE80, and PE100. It requires that the surface temperature deviation of the heating plate be less than 7℃, the porosity on the welding surface must not exceed 0.4 times the material thickness, and 10% of the joint needs to be sampled for slicing inspection. The DVS 2207-14 standard for welding polypropylene and polyethylene plates further refines the heating methods based on the plate thickness. For plates with a thickness of less than 6mm, single-side heating is allowed (with a temperature 5-10℃ higher than the conventional one), while for plates with a thickness of 6mm or more, simultaneous heating on both sides is required to ensure uniform heating. In the video of the 400PPH pipe hot melt welding machine customized by Saemin for a Chinese customer, the customer requested to use the German DVS standard.
In terms of domestic standards, GB/T 32434-2015 "Hot-melt Butt Welding Procedure for Polyethylene Pipes and Fittings for Gas and Water Supply Distribution Systems" is precisely adapted to the local gas and water supply pipeline scenarios. It clearly stipulates that the heating temperature for PE80 material is 210±10℃, and for PE100 material, it is 225±10℃. The heat absorption time is calculated as "wall thickness ×10 seconds". The cooling time is implemented as "wall thickness ×1.5 minutes", providing clear guidance for the welding of PE pipes with nominal outer diameters ranging from 75 to 630mm. The special standard HG/T 5100-2016 for the chemical industry focuses on the hot melt welding machine equipment itself, stipulating the pressure parameters of the oil cylinder for welding PE pipes of different diameters, such as 2.7×0.1MPa for DN63mm pipes and 17.0×0.1MPa for DN160mm pipes, to ensure the welding safety of chemical fluid transportation pipelines.
Industry experts say that the standardized operation of hot melt welding is the key to avoiding risks such as joint leakage and fracture. Enterprises and construction units need to precisely match the corresponding standards and parameters in combination with the requirements of the project area, the material and specifications of the pipes. Saemin welding machine manufacturer will continue to update various standard interpretations and technical guidelines in the future to support the high-quality development of the industry.